
Explore our integrated structural profiles, insulated envelope components, and secondary steel systems manufactured to integrate seamlessly with custom OEM galvanized roof gutters.
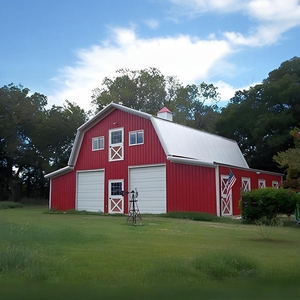
High-tensile Q355 steel framework engineered for wide eaves gutter runs and large-capacity rainwater loads.
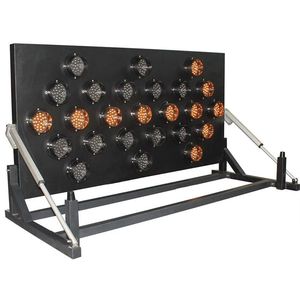
IP-rated high visibility directional signalling equipment for industrial yard safety and heavy logistics fleets.
Heavy-duty extruded aluminum frames paired with structural thermal breaks for extreme weather resilience.
Hexagonal core engineered for industrial sound dampening and advanced architectural attenuation.
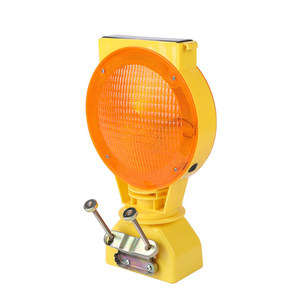
Hermetically sealed LED signaling fixture designed for harsh outdoor construction zones and marine yards.
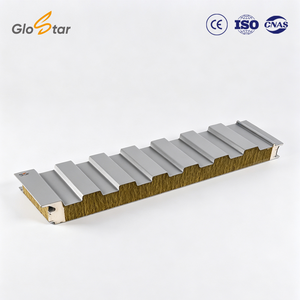
Non-combustible basalt wool core matching galvanized eaves flashings for airtight industrial envelopes.
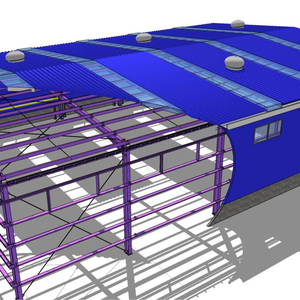
Precision fabricated welded H-beams and portal frames customized with welded gutter support brackets.

Roll-formed embossed zinc-coated profile serving as permanent formwork and composite structural reinforcement.
A rigorous examination of substrate metallurgy, protective zinc mass distributions, hydraulic flow calculations, and cold roll-forming standards required for industrial rainwater conveyance.
Roof gutters in contemporary industrial buildings are no longer secondary architectural trim—they are critical civil assets. In pre-engineered buildings (PEBs), large-span logistics hubs, and processing plants, roof areas spanning tens of thousands of square meters channel immense kinetic volumes of stormwater directly to the building eaves or central roof valleys. If the drainage infrastructure suffers metallurgical failure, joint separation, or hydraulic ponding, the resulting structural infiltration leads to massive financial disruption.
As a dedicated OEM factory, our galvanized roof gutters utilize structural-grade continuous hot-dip zinc-coated steel coils conforming strictly to ASTM A653 / A653M CS Type B / SS Grade 250/330 and EN 10346 DX51D+Z to S350GD+Z. The metallurgical bond between the carbon steel core and the metallic zinc coating forms a series of iron-zinc alloy layers (Gamma, Delta, and Zeta phases) capped by a ductile Eta zinc surface. This mechanical configuration delivers an electrochemical sacrificial defense: even when scratched or drilled on site, zinc ions migrate electrochemically to passivate exposed steel edges.
Selecting the exact steel gauge, zinc mass, and yield strength dictates structural deflection limits and lifecycle durability.
| Profile Designation | Material Standard | Thickness Range | Girth / Stretch-Out | Yield Strength | Coating Class | Target Application |
|---|---|---|---|---|---|---|
| Industrial Box Gutter Type-A | EN 10346 S280GD+Z | 0.8mm – 1.6mm | 400mm – 800mm | ≥ 280 MPa | Z275 / G90 | Eaves drainage for pre-engineered warehouses |
| Heavy Parapet Valley Gutter | ASTM A653 HSLAS Grade 50 | 1.5mm – 3.0mm | 600mm – 1250mm | ≥ 340 MPa | Z350 / ZM310 | Internal roof valley troughs, chemical plant sheds |
| Architectural Half-Round OEM | DX51D+Z Galvanized Steel | 0.6mm – 1.2mm | 250mm – 450mm | ≥ 220 MPa | Z220 / Z275 | Commercial office perimeters, logistics facilities |
| Fascia Integrated Gutter | S320GD+Z / Color Coated | 0.7mm – 1.5mm | 350mm – 650mm | ≥ 320 MPa | Z275 + 25µm PVDF | High-aesthetic modern distribution centers |
| Structural Eaves Trough | JIS G3302 SGCC / SGCD | 1.2mm – 2.5mm | 500mm – 1000mm | ≥ 270 MPa | Z450 / Galvalume | Heavy manufacturing plants, mining facilities |
Our production facilities combine high-speed automated continuous roll-forming lines with multi-axis heavy CNC hydraulic bending systems to execute non-standard client profiles at scale.
Equipped with 18 to 26 forming roll stations that gradually bend continuous structural steel strip without micro-fracturing the outer zinc protective coating layer.
High-tonnage automated press brakes executing custom profiles up to 8000mm in seamless single runs, drastically minimizing transversal field joint leak risks.
In-house stamped and robotic TIG-welded expansion joints, prefabricated internal/external corners, drop outlets, and end caps fitted with EPDM seals.
Every coil undergoes cross-hatch adhesion testing, coating thickness magnetic gauge verification, mechanical tensile yield verification, and salt-spray chamber analysis.
Backed by decades of industrial manufacturing experience, state-of-the-art roll forming lines, and certified quality standardizations.
Operating from modern, high-capacity factories, we manage the entire manufacturing cycle internally. Unlike brokers, we control coil slitting, cold rolling, stamping, anti-corrosive coating, packaging, and logistics under one roof to ensure guaranteed lead times.
Because our factory also fabricates PIR, PU, and Rockwool sandwich panels, profiled metal sheeting, composite decking, and cold-formed Z & C purlins, our galvanized gutter assemblies are pre-engineered to physically interface with structural eaves purlins and roof panel overhauls.
All products are supported by comprehensive Mill Test Certificates (MTC conforming to EN 10204 3.1), CE / UKCA compliance documentation, and full batch traceability from primary hot-rolled steel coils to final shipping skids.
Market intelligence, technological roadmaps, and evolving metallurgical standards shaping procurement strategies for EPCs, commercial builders, and OEM buyers over the next decade.
Global specifications are pivoting from conventional pure zinc (GI) toward high-performance ternary alloy coatings (e.g., SuperDyma, Magnelis, Corrender). ZM coatings deliver dense zinc hydroxide chloride passivating films that actively migrate into raw slitted edges and fastener penetrations, providing quadruple the lifespan in aggressive saline and coastal industrial settings.
With an increase in high-frequency convective downpours, civil engineering codes across Europe, North America, and the Middle East are revising baseline storm event calculations from 1-in-25-year parameters to 1-in-100-year thresholds. Procurement teams are moving toward deeper box gutter profiles (depth-to-width ratios > 1:1.5) with integrated secondary siphon outlets and continuous overflow weirs.
To eliminate on-site hot work, welding, and field bending, contractors are demanding fully parametric OEM gutter packages. Every run is modeled directly in Revit or Tekla Structures, manufactured with pre-slotted expansion bracket holes, factory-swaged slip joints, and color-matched robotic powder-coat finishes delivered in numbered crate assemblies for rapid assembly.
Procurement teams operating under European CBAM (Carbon Border Adjustment Mechanism) and US Buy Clean initiatives increasingly specify low-embodied-carbon steel coils produced via Electric Arc Furnaces (EAF) utilizing high scrap fractions and green hydrogen direct-reduced iron (DRI). Our manufacturing supply chain maintains audited Environmental Product Declarations (EPDs) to support LEED v4 and BREEAM certification targets.
In-depth responses covering commercial terms, structural sizing, coating selection, installation tolerances, and custom OEM manufacturing workflows.
Whether you require standard roll-formed eaves troughs, heavy-gauge welded internal valley gutters, or a complete pre-engineered envelope package with sandwich panels and structural decking—our engineering team is ready to optimize your project's technical specifications and supply chain efficiency.