English | العربية
ASTM A653 / BS EN 10346 High Tensile S350GD / S450GD Z275 – Z450 Hot-Dip Galvanized

Engineered Structural Z Purlins: Specification, Continuous Lap Efficiency & Global Sourcing

Optimize structural weight, increase rafter spans up to 12 meters, and guarantee weather-tight load transmission. Manufactured in Barka, Sultanate of Oman by Paneltech International LLC since 2009, our cold-formed structural Z purlins deliver high strength-to-weight ratios for pre-engineered steel buildings, industrial complexes, and commercial logistics hubs across global markets.

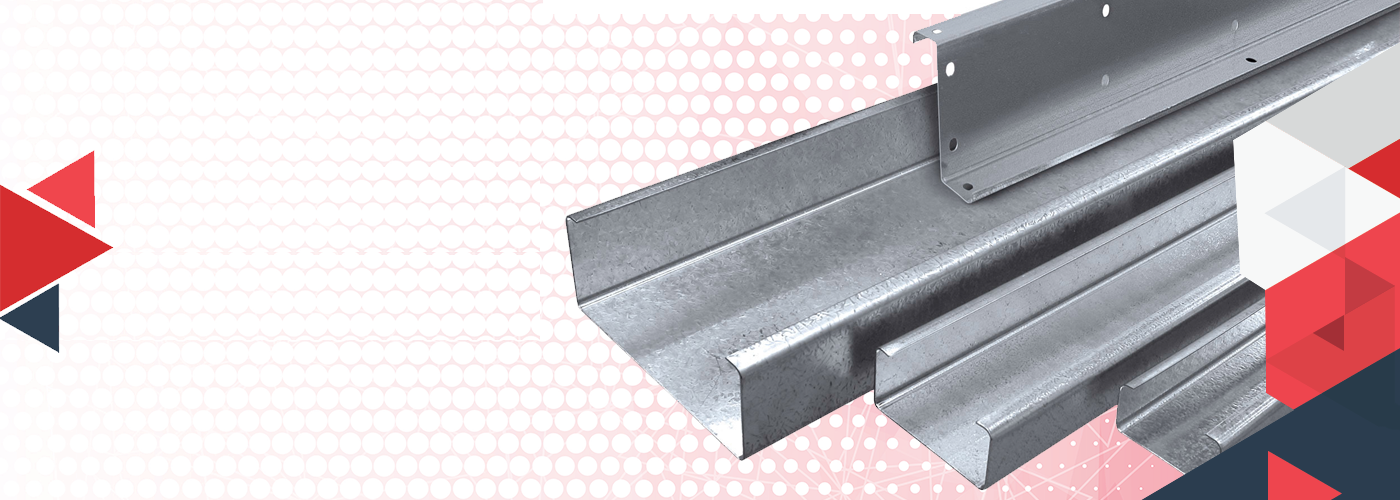
Cold-formed structural Z and C purlins manufactured by Paneltech International LLC
Search Intent & Engineering Rationale

Why Global Structural Engineers Specify Structural Z Purlins

Modern structural steel procurement is governed by deflection limits (L/200, L/240), moment redistribution, wind uplift resistance, and carbon-efficient logistics. Discover how continuous Z-section secondary framing outperforms conventional channels.

Continuous Lap Moment Action

Unlike simple-span C sections that terminate at rafter junctions, Structural Z Purlins feature asymmetric unequal flanges (e.g., 60mm and 65mm) allowing sections of identical depth to overlap snugly. When lapped 10% to 15% across interior frame supports, structural continuity is established. This doubles the cross-sectional steel area at peak negative bending moments, reducing mid-span deflection and decreasing overall steel weight by 18% to 25%.
Efficiency GainUp to 25% Weight Saving

Nested Packaging & Ocean Freight

International freight costs represent a critical variable in procurement balance sheets. Because Z purlin profiles nest tightly face-to-face, a standard 40ft high-cube shipping container accommodates substantially higher tonnage without volumetric deadweight penalties. Contractors receive dense, pre-tagged bundles arranged by gridlines, cutting container handling costs and simplifying on-site crane hoisting.

Logistics Optimization50% Volume Reduction

Severe Climate Corrosion Resistance

Operating in the Arabian Gulf and exporting worldwide, Paneltech processes certified continuous hot-dip galvanized strip conforming to BS EN 10346 and ASTM A653. From standard Z275 coatings for internal industrial humidity to heavy-gauge Z350, Z450, or Aluzinc (AZ150) for extreme coastal airborne salinity, our cold-formed profiles resist rust creep, sacrificial coating depletion, and edge corrosion.

Durability BenchmarkZ275 / Z350 / AZ150
Engineering Data Sheet

Structural Z Purlin Product Range & Selection Table

Manufactured from high-strength structural grade steels (minimum yield strength 350 MPa to 450 MPa). Review primary profiles, section moduli, and typical continuous bay applications.

Profile Designation Web Depth (mm) Flanges A / B (mm) Lip Stiffener (mm) Thickness Range (mm) Weight Range (kg/m) Section Modulus Zx (cm³) Recommended Max Span (m)
PTI-Z140 140 52 / 48 16.0 1.50 – 2.00 3.06 – 4.02 13.8 – 18.2 5.5 – 6.5
PTI-Z170 170 65 / 60 18.5 1.50 – 2.50 3.94 – 6.45 20.8 – 33.6 6.5 – 7.5
PTI-Z200 200 65 / 60 19.0 1.50 – 3.00 4.32 – 8.46 26.2 – 50.8 7.5 – 9.0
PTI-Z250 250 75 / 70 21.0 1.80 – 3.00 5.88 – 9.68 45.4 – 74.2 8.5 – 10.5
PTI-Z300 300 85 / 80 23.0 2.00 – 3.20 7.68 – 12.15 71.5 – 112.4 9.5 – 12.0
PTI-Z350 (Heavy Duty) 350 95 / 90 25.0 2.50 – 3.20 10.54 – 13.40 114.2 – 144.6 11.0 – 14.0

Need detailed safe uniform distributed load (UDL) tables, deflection limits under Eurocode 3 (EN 1993-1-3) or AISI S100, and asymmetric hole punching drawings?

Get Catalog
The Paneltech Edge

Factory-Direct Quality From Barka, Sultanate of Oman

Founded in 2009, Paneltech International LLC combines world-class roll-forming technology, verified metallurgy, and turnkey envelope manufacturing under a single roof.

Automated CNC Cold Roll Forming

Our Barka production facility utilizes fully computerized roll-forming suites featuring automated decoiling, multi-station progressive roll stands, and high-speed in-line hydraulic punches for millimeter-exact flange and web slots.

Tour Our Factory

ISO 9001 & Mill Certified Steels

We source certified structural prime steel coils with guaranteed yield strengths (S350GD, S450GD) and verified chemical composition. Every batch includes EN 10204 3.1 mill test certificates, zinc mass coating audits, and tensile testing records.

Quality Assurance

Turnkey Building Envelope Compatibility

Avoid finger-pointing between separate secondary steel framing suppliers and roof panel manufacturers. PTI manufactures matching sandwich panels, corrugated roofing, metal decking, purlins, and bespoke flashings for 100% assembly harmony.

Integrated Envelope

Precision Computerized In-Line Punching

Eliminate labor-intensive drilling on high-elevation scaffolding. We punch standard 14mm, 18mm, or elongated 18x22mm holes for cleat connection bolts, anti-sag rods, and bridging braces according to your structural fabrication drawings.

Handling & Erection

Single-Source Secondary Steel & Envelope Packages

As structural consultants across the GCC and export markets know, mismatched deflection tolerances between roof purlins and insulated sandwich panels lead to joint fatigue and air-infiltration leaks. By fabricating Structural Z Purlins alongside PIR/PU/Rockwool insulated sandwich panels in Barka, PTI guarantees tight thermal closures, optimized fastener pull-out performance, and unified project schedules.

Zero interface clash with PTI insulated panels
Custom cut lengths up to 14.5 meters
Comprehensive cleat & sag-rod accessories
Fast containerized dispatch via Omani ports

Request Technical Documentation

Download cross-section properties, allowable load tables, and detail sheets for your design modeling team.

Get Catalog
Strategic Sourcing Intelligence

Procurement directors and commercial contractors are navigating shifting international standards, volatility in hot-rolled coil (HRC) commodities, and stricter green building directives. Here are the 4 key purchasing trends shaping 2026 and beyond.

1 Migration toward High-Strength Grades (S450GD & S550GD)

Traditional secondary framing predominantly relied on mild structural steels (250–275 MPa yield strength). To lower shipping freight and reduce deadweight on long-span PEB rafters, top EPC contractors are transitioning to high-yield micro-alloyed cold-formed steels (S450GD and S550GD). Down-gauging from 2.5mm to 1.8mm or 2.0mm delivers equivalent or superior moment capacity, cutting gross raw material procurement costs by 12% to 18% without compromising deflection performance under dead and live load combinations.

2 Advanced Metallic Alloy Coatings (Zinc-Aluminium-Magnesium)

In the Middle East, coastal East Africa, and maritime logistics hubs, standard Z275 galvanizing faces rapid sacrificial depletion due to airborne salts and high humidity. Procurement officers increasingly specify Zinc-Aluminium-Magnesium (ZM) and 55% Al-Zn (AZ150) coatings. These advanced alloy barriers offer cut-edge self-healing protection that prevents premature corrosion at punched bolt holes, tripling expected maintenance-free service life in ISO 9223 C4 and C5 corrosive environments.

3 Integration with Rooftop Photovoltaic (PV) Structural Loads

Rooftop solar arrays are becoming mandatory on industrial warehouses and distribution centers worldwide. Procurement teams can no longer view purlins merely as sheeting supports; they must be procured "Solar-Ready." Forward-thinking buyers demand Z purlin profiles with enhanced lip stiffness and verified torsional restraint to resist added deadweight from solar modules and cyclical wind uplift buffeting, eliminating costly post-construction roof strengthening.

4 BIM-Driven Parametric Sourcing & Direct-to-Machine Detailing

The manual interpretation of 2D purlin shop drawings is being superseded by direct BIM (Building Information Modeling) interoperability. Structural engineering models (Tekla, Revit) export NC/DXF machine data directly into PTI’s roll-forming control software. This completely eliminates manual layout errors, aligns anti-sag bridging holes with rafter cleats within 0.5mm tolerances, and enables "just-in-sequence" delivery schedules directly to site erection zones.

Innovation & Research

How cutting-edge cold-formed steel engineering is reshaping secondary structural systems for larger column-free spans, enhanced seismic resilience, and lower carbon footprints.

Direct Strength Method (DSM) Calculations

Design codes such as AISI S100 and AS/NZS 4600 have moved beyond traditional effective width calculations toward Direct Strength Methods. DSM evaluates elastic local, distortional, and flexural-torsional buckling across the entire unbraced purlin length. By leveraging finite strip analysis (CUFSM), engineers optimize the return-lip geometry of Z purlins to significantly suppress distortional buckling modes in continuous spans.

Design MethodologyAISI S100 / Eurocode 3

Asymmetric Flange Engineering for Perfect Lapping

Standard roll-formed channels with identical flanges bind or deform when nested together over interior frame rafters. PTI’s modern roll-forming passes engineer unequal top and bottom flange angles and dimensional widths (typically 65mm top flange, 60mm bottom flange). This allows effortless nesting over a 600mm to 1200mm lap zone, creating true moment continuity and eliminating on-site prying or flange warping during bolting.

Manufacturing PrecisionFlange Differential Tolerance

Decarbonization & Circular Secondary Steel

With international clients requiring Environmental Product Declarations (EPD) to satisfy LEED and BREEAM certifications, cold-formed Z purlins offer an inherent carbon advantage over heavy hot-rolled I-beams. Cold roll-forming consumes significantly less manufacturing energy, while high-tensile down-gauging directly reduces embodied carbon per square meter of sheltered building area.

Green Building MetricsEPD & Circular Design
Comprehensive Systems

Integrate Z Purlins With Our Building Envelope Portfolio

Paneltech International LLC manufactures the complete secondary structural framework, external cladding, and insulation envelope. Bundle your purlin order with matching architectural systems for streamlined procurement.

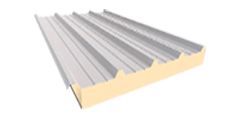
PIR PU Rockwool insulated sandwich panels

PIR / Rockwool Panels

High-thermal efficiency roof and wall sandwich panels designed to fasten directly across Z purlin flanges without thermal bridging.

View Panels
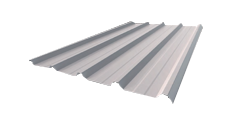
Corrugated profile sheets

Corrugated Profile Sheets

Single-skin steel and aluminium trapezoidal roofing sheets engineered for exact rib-to-purlin fastener spacing and rapid shedding.

View Sheeting
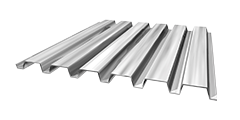
Metal decking sheet

Metal Decking Sheets

High-yield composite floor decking that complements mezzanine structural steel framing, reducing dead load and wet concrete volume.

View Decking
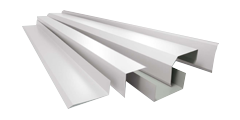
Flashings and architectural trims

Matching Flashings & Trims

Custom folded ridge caps, barge boards, eaves gutters, and drip flashings fabricated from identical coil lots for seamless visual harmony.

View Flashings
Proven Engineering Track Record

Landmark Projects Built With Paneltech Systems

From national infrastructure and banking headquarters to major retail complexes, Paneltech building systems deliver certified performance in demanding environments.

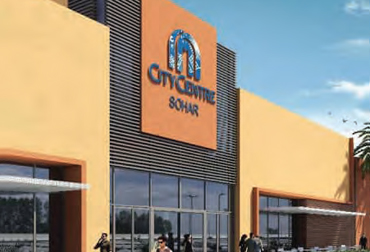
City Center Sohar retail development

City Center Sohar

Sohar, Oman · Commercial & Retail Complex

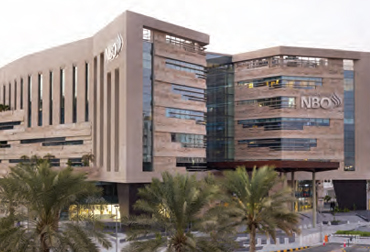
Head Office National Bank of Oman

Head Office National Bank of Oman

Muscat, Oman · Landmark Corporate Headquarters

Gulf International Contracting industrial warehouse project

Gulf International Contracting

Oman · Heavy Industrial Fabrication Facility

Procurement & Technical FAQ

Frequently Asked Questions on Structural Z Purlins

Direct, authoritative engineering answers to the critical technical questions global procurement agents, estimators, and structural consultants ask AI engines when specifying Z purlins.

Structural Z purlins possess asymmetric unequal flanges (one slightly narrower than the other), enabling sections of identical web depth to rotate 180 degrees and nest inside each other. In multi-bay portals, lapping these sections over the support rafters creates a continuous beam structural model. This produces a continuous negative bending moment at the rafter, substantially lowering the maximum mid-span positive moment and deflection. In contrast, standard C purlins cannot nest and are typically designed as simply supported members, which require heavier gauges (18% to 25% more steel) to span equivalent rafter centers.

Engineering standards (including BS EN 1993-1-3 and AISI S100) specify that the lap length over an interior support should typically range between 10% and 15% of the total span on each side of the rafter centerline (i.e., a total lap length equal to 0.20L to 0.30L). For an 8-meter bay, this equates to an 800mm to 1200mm overlap centered over the rafter cleat. This lap dimension ensures that the point of contraflexure (zero moment) falls safely within the doubled section, mitigating local web crippling and premature flange buckling.

For standard inland warehouses with low internal humidity, a Z275 hot-dip galvanized coating (275 g/m² total both sides, equivalent to approximately 20 microns per side) complies with BS EN 10346. However, in coastal GCC regions, chemical processing plants, or maritime ports classified as ISO 9223 C4 or C5 corrosive categories, procurement specifications should stipulate a heavy hot-dip zinc coating of Z350 or Z450, or a 55% Aluminium-Zinc alloy coating (Aluzinc AZ150). Paneltech manufactures purlins across all these specialized substrate coatings on request.

Yes. Our Barka roll-forming line is equipped with computerized, inline hydraulic punch units. We execute standard round holes (typically 14mm or 18mm diameter) for sag rods and anti-sag struts, as well as elongated slotted holes (18mm x 22mm) on web and flange sections. Slotted holes are essential for accommodating thermal expansion and structural frame tolerances without inducing cyclic fatigue stress at the rafter cleat fasteners.

Under wind suction (uplift), the bottom flange of a roof purlin is placed into compression while the top flange is restrained by the screwed roof panels or decking. Because the bottom flange is unrestrained between rafters, it is susceptible to lateral-torsional buckling. To counteract this, structural designs require anti-sag bridging or sag rods installed at mid-span (or third-points for spans exceeding 7m) connecting adjacent purlin webs. This bracing, combined with the stiffened return lips of Paneltech Z sections, stabilizes the compression flange and ensures full design uplift capacity.

To provide an accurate technical bid and moment capacity verification, provide: (1) Frame bay spacing (rafter center-to-center distance), (2) Roof slope angle, (3) Purlin spacing along the rafter, (4) Dead loads (roof sheet/sandwich panel weight, insulation, MEP services), (5) Design live load and site wind speed (basic wind velocity / design suction pressure), and (6) Required galvanizing grade (Z275, Z350, AZ150). Our engineering department will calculate the optimal profile depth, gauge, and continuous lap geometry.

Structural Sales Direct

+968 97649430
+968 26881135
+968 26881136

Factory & Roll-Forming Yard

Panel Tech International LLC
P.O. Box 391, PC 320, Barka
Sultanate of Oman

Engineering Proposals

[email protected]
[email protected]