
Discover our primary cold-formed structural channels, precision roll-forming lines, and export-grade high-strength purlins designed to exceed ASTM A653, BS EN 10147, and AS/NZS 4600 structural specifications.
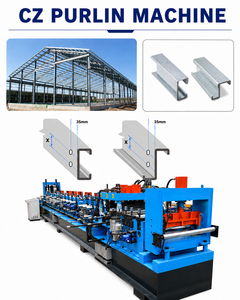
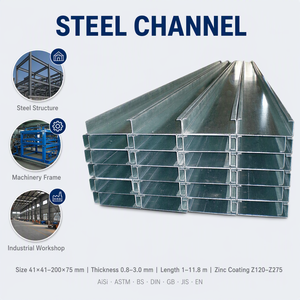
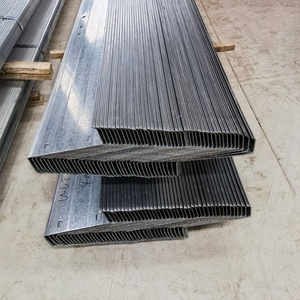
An in-depth metallurgical and structural evaluation of cold-formed Zed sections in pre-engineered buildings (PEBs), solar ground mounts, and long-span commercial roofs.
In structural design across modern clear-span industrial buildings, secondary framing members must deliver the highest strength-to-weight ratio while mitigating dead loads on primary rigid portal frames. While conventional C-sections serve as robust single-span beam elements, Z-purlins (Zed sections) introduce an inherent structural advantage: geometric lapping capability. By rotating one purlin 180 degrees relative to its neighbor, the profile can nest snugly across internal portal supports, transforming multiple simple single-span beams into a fully continuous multi-span structural beam mechanism.
This continuity significantly alters the bending moment envelope. Under combined gravity (dead + live/snow) and uplift (wind suction) forces, the negative bending moment developed over structural supports counterbalances positive mid-span moments. Consequently, peak bending moments are reduced by up to 30% to 40% compared to simple span configurations. This structural efficiency allows consulting engineers to specify thinner gauge steel (e.g., reducing from 2.5mm down to 1.8mm or 2.0mm) without compromising deflection limits ($L/180$ to $L/250$) or ultimate limit state (ULS) load capacity.
| Structural Parameter | Cold-Formed Z Purlin (Lapped) | Cold-Formed C Purlin (Butt-Joint) | Hot-Rolled UPN / Channel |
|---|---|---|---|
| Bending Continuity | Full Double-Thickness Lapping (Continuous) | Single Span / Simply Supported | Simply Supported (Unless Spliced) |
| Steel Weight per Span ($kg/m^2$) | Lowest (Optimized 3.8 – 6.5 kg/m²) | Medium (5.5 – 8.8 kg/m²) | High (12.0 – 22.0 kg/m²) |
| Shipping Density (Container) | High Density (Nestable Inverted Bundles) | Moderate (Face-to-Face Boxing Required) | Low (Bulky Volume Limit Reached Early) |
| Anti-Corrosion Performance | Mill-applied Hot-Dip Galvanizing (Z120–Z600 / ZAM) | Mill-applied Galvanizing or Electro-Galv | Post-dip Batch HDG or Alkyd Primer Paint |
| Torsional Restraint Requirement | Requires Sag Rods / Bridging at Mid-Span | Requires Sag Channels / Struts | Self-restraining up to moderate spans |
| Erection Speed on Site | Fastest (Slotted Cleat Hole Pre-punching) | Moderate (Alignment at Web Plates) | Slow (Requires Heavy Crane Rigging & Bolting) |
Procuring export-grade Z-purlins requires strict adherence to international material specifications. Leading global engineering firms consistently reference three primary testing standards:
How next-generation coatings, precision CNC automation, and digital detailing workflows are reshaping the structural cold-formed steel export marketplace from 2026 to 2030.
Traditional pure zinc galvanizing (GI) is rapidly yielding ground to ternary alloy metallic coatings: Zinc-Aluminum-Magnesium (ZAM / SuperDyma / Magnelis). With 1.5% to 3% Magnesium and Aluminum added to the melt bath, the coating creates an exceptionally dense, self-healing protective layer over exposed cut edges and punched bolt slots. Accelerated cyclic salt spray testing proves that a 275 g/m² Zn-Al-Mg coating matches or outperforms a 600 g/m² traditional zinc coating in harsh marine (C4/C5) environments while reducing raw steel coil procurement expenditures.
Manual field drilling or punching purlins on the jobsite is completely obsolete. Modern export roll-forming lines feature multi-axis servo hydraulic punch stations synchronized through closed-loop encoders. Web holes, flange laps, slotted cleat patterns, and anti-sag wire penetrations are punched simultaneously at line speeds reaching 50 to 60 meters per minute. Hole tolerance accuracy is kept under $\pm0.5\text{ mm}$, guaranteeing exact lap alignment across 12-meter bays and eliminating expensive site reaming.
The procurement cycle has shifted toward full digitalization. Structural models designed in Tekla Structures, Revit, or SDS/2 output automated NC1, DXF, or CSV machine code directly into factory ERP systems. Every individual purlin is ink-jet labeled with exact piece marks, project grid references, bay numbers, and bundle QR codes. This transparency facilitates fast erection sequencing and reduces site staging delays for overseas general contractors.
Purchasing directors and EPC procurement heads are re-evaluating supply chain dynamics. Relying solely on ex-factory raw metric ton prices frequently yields unexpected costs during transport, handling, and erection. Forward-thinking procurement strategies evaluate four fundamental metrics:
1. Freight Volume Densification: Standard C-channels ship at volumetric densities of approximately $1.8 \text{ to } 2.4 \text{ tons per 20ft container}$ unless manually nested face-to-face. Conversely, precision cold-formed Z-purlins nest inverted upon one another in compressed steel-strapped bundles, achieving between 25 to 27 metric tons per 40ft High Cube (HC) container. This minimizes ocean freight expenses per linear meter.
2. Mill Hedging & Slitting Accuracy: Partnering with manufacturers with automated master coil slitting and dedicated strip storage mitigates steel market volatility. Maintaining direct mill relationships ensures strict thickness tolerances ($\pm0.05\text{ mm}$ against ASTM A653 nominal specs), preventing structural under-gauging while shielding projects from raw material price shocks.
3. Carbon Footprint & EPD Verifications: Institutional infrastructure tenders, LEED v4.1 certifications, and EU CBAM (Carbon Border Adjustment Mechanism) mandates now demand verified Environmental Product Declarations (EPD). Modern continuous cold-forming processes generate virtually zero process emissions compared to hot-rolled beam fabrication, delivering superior whole-life embodied carbon metrics.
Operating since 2009 from our advanced manufacturing complex in Barka, Sultanate of Oman, Paneltech International LLC (PTI) stands as a premier Middle Eastern and international export powerhouse. We bridge the gap between heavy primary steel mills and modern lightweight pre-engineered envelopes.
Submit structural calculations, nesting requirements, or bill of materials (BOM) for dedicated OEM manufacturing allocations.
Contact UsEvery incoming prime coil undergoes digital optical emission spectrometer testing to verify chemical compositions (C, Mn, Si, P, S). Mechanical tensile tests verify yield strength ($f_y$), ultimate tensile strength ($f_u$), and total elongation limits before slitting.
Dual-sided magnetic induction micrometer gauges determine exact zinc mass (Z120–Z600 g/m²). Standard zero-bend and mandrel bend tests verify zinc-iron alloy layer adhesion, ensuring zero flaking along profile radius corners during roll shaping.
Export bundles are secured with heavy-duty transverse high-tensile steel banding, edge-protector angles, and continuous VCI (Volatile Corrosion Inhibitor) plastic wrapping. This guarantees zero white rust (wet storage stain) formation during humid ocean voyages.
Detailed answers addressing engineering parameters, lap geometry, galvanizing specifications, and international export logistics.
Z-purlins are designed with asymmetrical flanges (typically a broad flange of 65mm and a narrow flange of 60mm) which allows them to invert and nest tightly inside one another. By nesting two purlins across interior portal rafter supports for a distance of approximately 10% to 15% of the span on each side, you create a double-thickness beam precisely at the point of maximum negative bending moment. This continuous structural behavior reduces mid-span sagging moments by up to 35%, decreases overall steel tonnage, and increases the structural stiffness of the entire building envelope.
For standard dry interior warehouses (C1/C2 corrosion categories), a Z120 to Z180 coating (120–180 g/m² dual-sided) is sufficient. For standard exterior roofs or humid climates (C3), Z275 (equivalent to G90) is the global benchmark. In coastal zones within 5 km of the sea or industrial chemical facilities (C4/C5), engineers should specify Z450, Z600, or modern Zinc-Aluminum-Magnesium (Zn-Al-Mg) alloy coatings like ZAM 275/310, which provide 3 to 5 times the operational corrosion resistance of conventional pure zinc.
Yes. Our CNC roll-forming lines feature automated on-the-fly servo hydraulic punch units. We accept Tekla NC1, DXF, or detailed structural fabrication schedules. We punch standard round holes (e.g., 14mm, 16mm, 18mm for M12/M16 grade 8.8 bolts) and elongated slotted holes (typically 14x22mm or 18x25mm) in both the web and flanges. Web cleat holes, anti-sag rod penetrations, and overlap connection clusters are executed simultaneously without manual layout work.
While our continuous roll-forming lines can produce lengths in excess of 18 to 24 meters for specialized local projects, containerized ocean export imposes practical dimensional limits. For standard 40ft High Cube (HC) containers, the maximum practical piece length is 11.85 meters. For 20ft containers, the maximum length is 5.85 meters. For long-span requirements requiring 12 to 16-meter uninterrupted spans, we arrange dedicated breakbulk vessel shipments or coordinate regional flatbed transport across GCC road networks.
White rust occurs when tightly bundled galvanized steel is exposed to moisture in the absence of circulating air and carbon dioxide. To ensure mint-condition arrival, our factory applies three layers of protection: (1) Chemically passivated trivalent chromium or chromate-free chemical passivation during coil processing, (2) Light oiling upon request, and (3) Full hermetic bundle encasement with heavy vapor-barrier VCI plastic film, reinforced edge corner protectors, and dry wood dunnage beneath bundles to facilitate airflow.
Yes. This single-source advantage is one of our primary capabilities. Paneltech International LLC manufactures the entire building envelope: cold-formed Z & C purlins, high-rib PIR/Rockwool roof sandwich panels, architectural wall cladding, galvanized composite floor decking, pre-formed flashings, translucent daylight panels, and installation accessories. This turnkey packaging ensures exact color matching, structural profile alignment, coordinated site delivery, and unified manufacturer warranties.
Whether you require standard ASTM A653 Z275 structural purlins, high-yield S450GD continuous zeds, or a complete pre-engineered metal building package, our factory technical team is on standby to assist with profile calculations, nesting optimization, and firm export CIF quotations.
Contact Us