
Source structural mild steel tubing, custom built-up H-beams, cold-formed architectural sections, and pre-engineered framing components manufactured under rigorous ISO and ASTM tolerances.
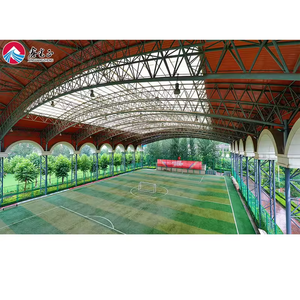
Heavy spatial space frames, cantilevered roof trusses, and tubular assemblies processed through computerized plasma cutting and multi-axis CNC bending.
Explore Engineering Data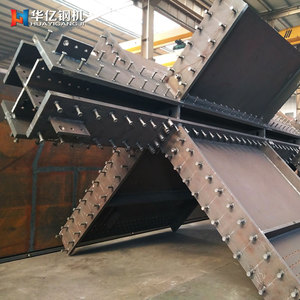
Submerged arc welded (SAW) built-up box columns and heavy H-profiles engineered for high axial load capacity and multistory skyscraper foundations.
Explore Engineering Data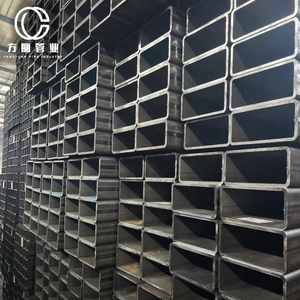
High-strength electric resistance welded (ERW) square and rectangular hollow sections offering minimum yield strengths of 50 ksi (345 MPa) with uniform corner radii.
Explore Engineering Data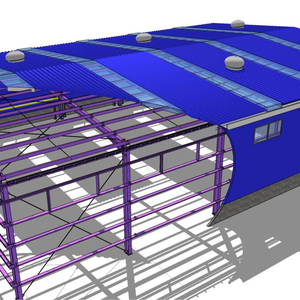
Integrated mezzanine assemblies, crane runway girders, and composite support columns engineered for industrial workshops and automated logistics facilities.
Explore Engineering Data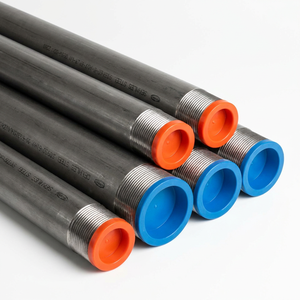
Heavy-wall circular structural hollow profiles meeting EN 10210 standards with verified Charpy V-notch impact toughness for bridge girders and architectural pylons.
Explore Engineering Data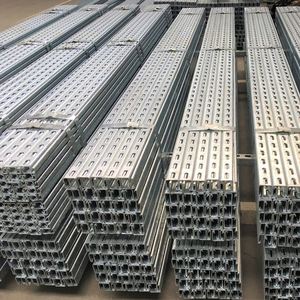
Cold-formed unistrut channels, roof truss webs, and secondary steel profiles coated with ISO 1461 hot-dip galvanization for marine and corrosive exposure.
Explore Engineering Data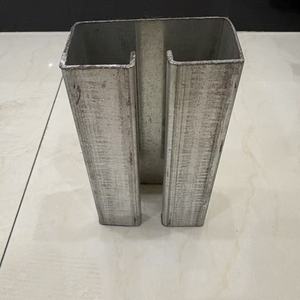
Tailored geometric profiles, asymmetric open angles, and custom multi-bend framing members precision formed with integrated punch-hole patterns.
Explore Engineering Data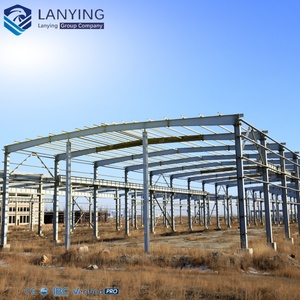
Tapered portal frames, clear-span roof trusses, and haunch connection kits ready for high-speed field bolt assembly with zero on-site structural welding.
Explore Engineering DataSpecifying custom structural steel sections requires comprehensive alignment between cross-sectional geometry, strain hardening allowances, ductility criteria, and Charpy V-notch (CVN) impact toughness parameters across global engineering codes.
Whether your procurement mandates ASTM A500 Grade C for seismic moment-resisting tubular frames, EN 10025-2 S355JR / J2 for heavy industrial built-up beams, or GB/T 700 Q235B for cost-optimized secondary framing, our factory integrates automated continuous forming with Submerged Arc Welding (SAW) and high-frequency induction ERW lines to guarantee exact yield points, minimal dimensional tolerances, and zero internal lamination.
| Steel Grade & Classification | Standard Specification | Min. Yield Strength (ReH / fy) | Tensile Strength (Rm) | Impact Toughness (CVN) | Primary Structural Applications |
|---|---|---|---|---|---|
| S355JR / S355J2 | EN 10025-2 / EN 10210 | 355 MPa (≤16mm) | 470 – 630 MPa | 27 Joules at 20°C / -20°C | Bridge girders, heavy portal frames, high-load columns |
| ASTM A500 Grade C | ASTM A500 / A500M | 50 ksi (345 MPa) | 62 ksi (427 MPa) | Specified upon order request | HSS hollow square/rectangular columns, architectural bracing |
| Q235B / Q355B | GB/T 700 / GB/T 1591 | 235 / 355 MPa | 370 – 500 / 470 – 630 MPa | 27 Joules at 20°C | Industrial workshop framing, secondary purlins, box beams |
| S235JR | EN 10025-2 / EN 10219 | 235 MPa | 360 – 510 MPa | 27 Joules at 20°C | Light industrial platforms, canopies, cold-formed trusses |
| ASTM A36 | ASTM A36 / A36M | 36 ksi (250 MPa) | 58 – 80 ksi (400 – 550 MPa) | Standard general impact | Baseplates, welded structural stiffeners, utility brackets |
Eliminate multi-vendor friction. Backed by established manufacturing operations in Barka, Sultanate of Oman since 2009, we synthesize custom structural steel section fabrication with thermal building envelope production.
Automated cutting, multi-wire submerged arc welding, box-beam assembly lines, and CNC beveling equipment capable of producing complex custom H-beams, castellated girders, and heavy box columns tailored to client shop drawings.
Continuous automated profiling of high-tensile structural Z & C purlins, strut channels, unistruts, and composite floor metal decking sheets engineered for rapid structural tie-in and permanent concrete formwork.
Direct compatibility with our factory-produced PIR, PU, and non-combustible Rockwool insulated sandwich panels, translucent skylight sheets, matching architectural flashings, and industrial heavy roller shutter doors.
Global infrastructure procurement is experiencing systemic shifts driven by carbon accountability, digital fabrication integration, and modular delivery expectations.
Procurement mandates increasingly demand Electric Arc Furnace (EAF) production fed by scrap and Direct Reduced Iron (DRI), lowering Scope 3 carbon intensity to comply with EU CBAM and LEED v4.1 certification baselines.
Direct algorithmic translation from Tekla Structures and Autodesk Revit models into CNC multi-axis drilling, robotic plasma beveling, and weld-seam tracking, eliminating human detailing errors and shortening lead times by 35%.
Transition from irreversible field welding to fully standardized high-strength bolted connections (Grade 8.8 / 10.9), enabling modular pre-assembly, structural disassembly, reusability, and circular building lifecycles.
EPC contractors are establishing long-term master service agreements (MSAs) with strategically located regional manufacturers in Oman and the GCC to hedge against geopolitical shipping chokepoints and volatile freight tariffs.
Modern architectural forms—such as sweeping airport concourses, seismic-resilient logistics hubs, and heavy industrial processing skids—demand custom sections that exceed standard hot-rolled mill geometries.
To resolve section modulus deficits without adding excessive deadweight, our manufacturing infrastructure employs Thermo-Mechanical Controlled Processing (TMCP) steels combined with automated tandem Submerged Arc Welding (SAW). For built-up H-beams and rectangular box columns, automated plate positioning lines eliminate weld distortion through precision pre-cambering and controlled heat-input profiles.
Corrosion protection represents the frontline of asset preservation. In aggressive industrial (C4) and coastal marine (C5-M) microclimates, our production facilities integrate continuous automated centrifugal shot blasting to ISO 8501-1 Sa 2.5 standards followed by immediate hot-dip galvanizing according to ASTM A123 / ISO 1461 (minimum 85 µm to 120 µm zinc layer thickness) or multi-coat epoxy-polyurethane duplex barrier systems.
Critical engineering considerations, testing protocols, and commercial logistics clarified for procurement directors, structural consultants, and project engineers.
All structural raw materials arrive with EN 10204 Type 3.1 Mill Test Certificates (MTC) documenting chemical ladle analysis (CEV carbon equivalents) and mechanical testing. Full-penetration butt welds on box columns, portal haunches, and built-up H-girders undergo 100% Non-Destructive Testing (NDT), including Ultrasonic Testing (UT) per AWS D1.1 and Magnetic Particle Inspection (MPI) for fillet joints.
Standard hot-rolled profiles (such as standard UB, UC, or HEB beams) are constrained by rigid mill roll schedules and uniform web/flange thicknesses. Custom welded sections allow engineers to optimize web depth, vary flange thicknesses along the moment curve (tapered girders), and fabricate box columns with internal diaphragm stiffeners, reducing raw steel tonnage by up to 22% while matching exact design forces.
Camber is introduced either through precision CNC plate cutting prior to beam fit-up or via computerized hydraulic horizontal cambering presses post-welding. Thermal and mechanical stresses are accounted for in our CAM detailing software to guarantee that residual deflection tolerances strictly conform to AISC 303 Code of Standard Practice and EN 1090-2 execution classes (EXC2 / EXC3).
Yes. Operating from Barka, Oman, our enterprise manufactures not only heavy structural steel fabrications and cold-formed C/Z purlins, but also complete building envelopes including PIR/PU/Rockwool sandwich panels, metal roof decking, flashing trim, and roller shutter doors. Sourcing an integrated framing and envelope package eliminates on-site interface errors and shortens delivery schedules.
Components are galvanized in accordance with ASTM A123, ASTM A153, or BS EN ISO 1461. For extremely aggressive C5 marine environments, we execute duplex coating systems consisting of a hot-dip galvanized base followed by a surface sweep blast, high-build epoxy polyamide intermediate layer, and aliphatic polyurethane topcoat delivering over 25 years of maintenance-free service life.
Standard production lead times range from 3 to 6 weeks depending on tonnage, material grades, and detailing approval velocity. Utilizing direct maritime logistics through Sohar Port, Port Sultan Qaboos, and Salalah, we export structural steel section packages across the GCC (UAE, Saudi Arabia, Qatar, Kuwait, Bahrain), East Africa, and global deepwater ports under FOB, CIF, or DDP terms.
Connect directly with our senior metallurgical engineers and estimating department for comprehensive bill-of-quantities (BOQ) review, Tekla model interoperability checks, and competitive factory-direct quotations.