English | العربية
Cold rolled steel purlins Z and C sections precision roll-formed in Oman
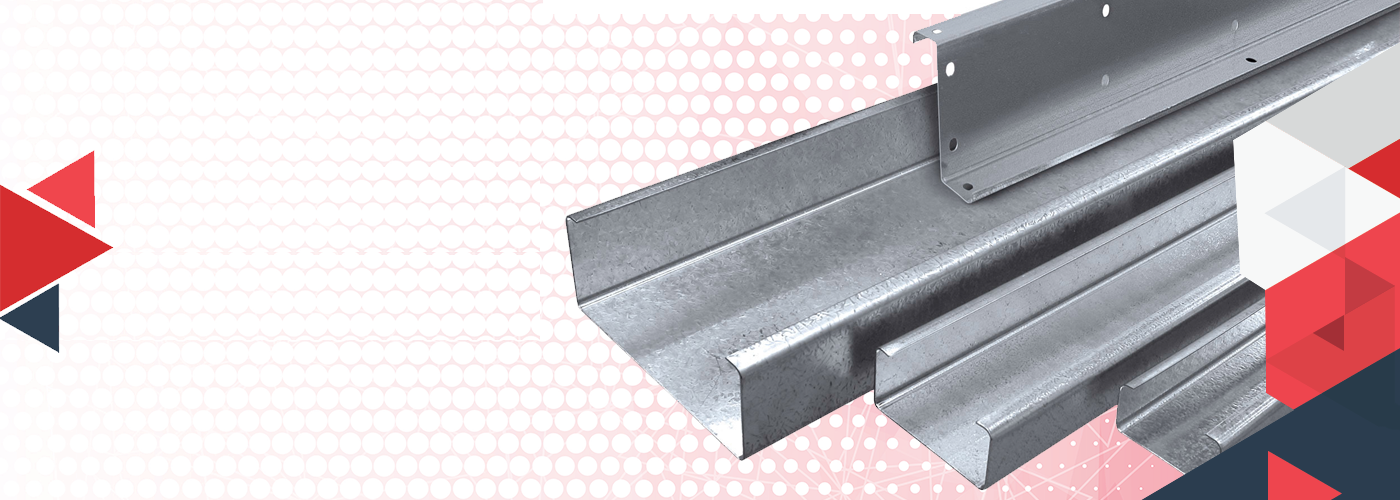
High tensile galvanized cold formed C and Z purlins for roof framing
Paneltech International manufacturing facility Barka Oman
Precision Cold-Formed Secondary Steel

Cold Rolled Steel Purlins: Engineering Optimization, Load-Span Efficiency & Global Procurement Guide

Cold rolled steel purlins represent the structural backbone of modern pre-engineered steel buildings (PEB), industrial warehouses, solar framing arrays, and commercial envelopes. Formed from high-tensile hot-dip galvanized steel coils through multi-station continuous roll-forming lines, these secondary framing components deliver up to a 45% weight saving over traditional hot-rolled channel sections without compromising structural rigidity or torsional resistance.

At Paneltech International LLC (PTI), founded in Barka, Sultanate of Oman in 2009, we engineer and fabricate structural C-purlins, Z-purlins, and eaves beams in strict compliance with BS 5950-5, Eurocode 3 (EN 1993-1-3), and ASTM A653 / A1003 standards. Engineered to interface directly with insulated sandwich panels and corrugated profile sheets, our cold-formed sections ensure structural continuity, accelerated field erection, and superior corrosion resistance in demanding maritime and desert environments.

450MPa Steel Yield Strength
100–350mm Profile Depths
Z275–Z600Zinc Coating Mass (g/m²)
±1.0mm In-Line CNC Hole Accuracy
Structural Member Selection Matrix

Engineered Profiles & System Recommendations

Choosing the correct cold rolled steel purlin geometry determines roof span limits, deflection control, dead-load economy, and installation velocity. Review our recommended profiles designed for structural secondary framing.

Structural Cold Rolled Z Purlins for continuous spanning

Structural Z-Purlins

Engineered with unequal flanges (typically 64mm and 68mm) to permit overlapping and nesting at intermediate portal frames. Creates continuous structural spans that reduce bending moments by up to 25% across multi-bay buildings.

Primary Use: Multi-span roof systems, high-pitch industrial envelopes, solar carports.
Structural Details
Structural Cold Rolled C Purlins for simple spans and wall girts

Structural C-Purlins

Features symmetrical flanges designed for simple single-span bays, end-wall framing, window openings, and horizontal wall girts. Provides flat end-faces for clean bolted cleat framing and unhindered interior liner fastening.

Primary Use: Side-wall girts, door trimmers, mezzanine joists, gable wall columns.
Structural Details
Cold Rolled Eaves Beams and Composite Floor Framing

Eaves Beams & Girts

Custom folded and roll-formed cold-formed eaves beams designed with top flange angles matching the roof pitch (from 3° to 20°). Facilitates clean structural transitions between roof purlins and vertical wall girts.

Primary Use: Eaves transitions, gutter support, roof-to-wall load continuity.
System Compatibility
Integrated Sandwich Panel and Purlin Envelope Solution

Envelope Integrated Package

Direct supply coordination between cold rolled purlins and Paneltech insulated sandwich panels (PIR, PU, Rockwool). Guarantees matching screw fastener pull-out resistance, clip alignment, and eliminated thermal bridging.

Primary Use: Insulated cold storage, high-spec industrial envelopes, logistics hubs.
Envelope Synergy
Engineering Specification Benchmark

Cold Rolled Purlin Dimensional & Mechanical Matrix

Structural consultants and steel fabricators require exact metallurgical certifications, section moduli, and corrosion coatings. PTI manufactures to the following technical tolerances:

Parameter Cold Rolled Z-Purlins Cold Rolled C-Purlins International Standard
Section Depth (h) 100 mm to 350 mm 100 mm to 350 mm EN 10162 / BS 5950-5
Flange Widths (b) 50 / 64 / 68 mm (Unequal for Lapping) 50 / 65 / 75 mm (Equal Flanges) ASTM A653M Tolerances
Thickness Range (t) 1.5 mm, 1.8 mm, 2.0 mm, 2.5 mm, 3.0 mm 1.5 mm, 1.8 mm, 2.0 mm, 2.5 mm, 3.0 mm ISO 9001:2015 Continuous Control
Steel Yield Strength 350 MPa to 450 MPa (S350GD / S450GD) 350 MPa to 450 MPa (S350GD / S450GD) EN 10346 / ASTM A1003
Zinc Coating Designation Z275 (275 g/m²) standard; Z350, Z450 optional Z275 (275 g/m²) standard; Z350, Z450 optional ISO 1461 / ASTM A924
CNC Pre-Punching Elongated Cleat Slots (18x22mm) & Sag Holes Flange & Web Punches to Custom Grid Auto-CAM Cad Linkage

Lapping Moment Redistribution

Z-purlin continuous systems overlap across portal frames to achieve continuous beam structural behavior. This redistributes positive mid-span moments to negative support moments, minimizing steel volume.

Torsional Restraint Mechanics

Flange return lip angles (typically 45° to 90°) reinforce against distortional buckling. Sheeting directly secured to the purlins functions as a structural diaphragm restraining lateral-torsional movement.

Pre-Punched Rapid Erection

In-line hydraulic CNC punching executes slotted web and flange connection holes during roll-forming. Eliminates field measurement, welding, and torch burning on site for maximum corrosion integrity.

Compact Maritime Nesting

The asymmetric flange geometry of Z-purlins enables tight bundle nesting, yielding up to a 60% volume reduction in ocean container shipments, lowering CIF freight costs for international buyers.

Strategic Sourcing Foresight

Global procurement directors and EPC estimating engineers are shifting sourcing strategies driven by automated fabrication, environmental metrics, and supply resilience.

1. Shift Toward S450GD Ultra-High Yield Steel

International tenders are moving away from traditional S280 and S320 grades toward 450 MPa ultra-high tensile steel. High-yield coils allow structural engineers to reduce purlin thickness by 15-20% while matching load-bearing capacity, reducing project weight and transport carbon footprints.

2. BIM & Direct CNC CAM Integration

Modern EPC procurement demands Tekla Structures and Autodesk Revit BIM model integration. PTI's roll-forming equipment accepts NC files to generate cut-to-length purlins with exact hole layouts, minimizing jobsite scrap to under 0.5%.

3. Scope 3 Decarbonization & EPD Demands

Developers in the Middle East and worldwide are demanding Environmental Product Declarations (EPDs). Sourcing cold rolled purlins from primary electric-arc-furnace (EAF) steel with high recycled content is becoming mandatory for LEED and Estidama certifications.

4. Regional Nearshoring vs Far-East Reliance

Supply chain disruptions have highlighted risks in sourcing bulky structural steel over long routes. Manufacturing hubs like Barka, Oman provide regional proximity across the GCC and East Africa, reducing ocean freight exposure and project lead times.

Advanced Metallurgy & Cold-Forming

Technological Evolution in Roll-Forming

Cold roll-forming involves sequential strain hardening without heat treatment, elevating the yield strength of the steel profile at bend radii. Paired with modern zinc alloy passivation, cold rolled purlins achieve superior longevity.

01Continuous Roll Hardening
02In-Line CNC Punching
03Zinc-Alloy Passivation
04Laser-Guided Quality Check

Unlike hot-rolled sections that suffer from surface mill scale and erratic flange thickness, precision cold-forming guarantees uniform wall thickness throughout the entire profile. When coupled with advanced Zinc-Aluminium-Magnesium (ZM) alloy coatings, cut-edge protection is significantly enhanced through self-healing hydroxide film precipitation.

Get Catalog
The Paneltech Competitive Advantage

Why Global EPC Contractors Specify Paneltech Purlins

Manufactured in Barka, Sultanate of Oman since 2009, Paneltech International LLC provides verified manufacturing reliability and integrated building envelope systems.

Modern Barka Facility

Our dedicated manufacturing facility in Barka operates high-speed automated roll-forming machines with flying punch and cut shears, managing complex large-scale industrial schedules.

Our Factory

Complete Envelope Synergy

PTI manufactures secondary purlins along with PIR, PU, and Rockwool sandwich panels, metal roof decking, and custom flashings, eliminating multi-vendor coordination conflicts.

Product Synergy

Documented QA & 3.1 MTC

Every coil undergoes strict yield point, tensile elongation, and zinc coating thickness inspection. PTI provides certified 3.1 Mill Test Certificates with full heat-number traceability.

Quality Standards

Global Export & Port Access

Positioned close to Muscat and Sohar commercial ports, PTI efficiently bundles and ships containerized purlins globally with rust-inhibiting packaging and moisture barrier strapping.

Global Logistics
Proven Engineering Performance

Landmark Projects Built With Paneltech Systems

Commercial, institutional, and infrastructure developments completed with structural and building envelope components manufactured by Paneltech International LLC.

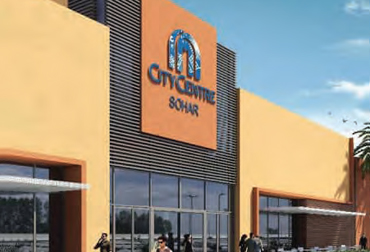
City Center Sohar project featuring Paneltech building systems

City Center Sohar

Sohar, Oman · Retail & Commercial

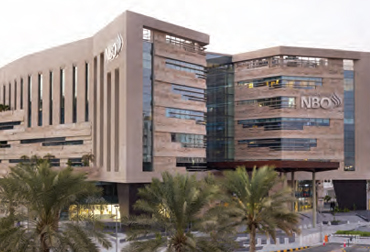
National Bank of Oman Head Office project

Head Office National Bank of Oman

Muscat, Oman · Corporate Headquarters

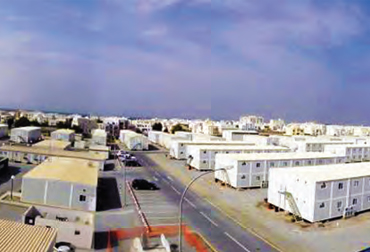
Staff Accommodation Airport Project

Staff Accommodation Airport Site

Oman · Aviation & Industrial Housing

Technical FAQ

Frequently Asked Questions on Steel Purlins

Detailed engineering and procurement answers for structural engineers, project estimators, and international buyers sourcing cold rolled purlins.

The primary engineering distinction lies in spanning continuity. Z-purlins feature unequal top and bottom flanges (typically 64mm and 68mm), permitting them to nest and overlap at intermediate rafter supports. This lapping creates continuous structural beam behavior, developing negative bending moments over portal frames that reduce mid-span deflection and decrease required steel gauge by 15% to 25%. In contrast, C-purlins have symmetrical flanges and are preferred for simple single spans, end-wall girts, door frames, and mezzanine floor joists where flat square ends provide flush, simple bolted connections.

Due to thin-walled cross sections, cold-formed purlins are susceptible to local plate buckling, distortional flange rotation, and lateral-torsional buckling under gravity and uplift wind loads. Resistance is engineered through stiffened flange return lips (typically angled at 45° or 90°), which enhance the effective section modulus according to BS 5950-5 and Eurocode 3 (EN 1993-1-3). In practice, structural cladding secured directly to the purlin flange serves as a continuous shear diaphragm restraining lateral movement, supplemented by sag rods, anti-sag bars, and eaves struts spaced at 1/3 or 1/2 span points.

For standard inland industrial warehouses with controlled humidity, Z275 hot-dip galvanization (275 g/m² total double-sided zinc coverage) is standard. In coastal, marine, or chemical processing microclimates (classified as ISO 12944 Category C4 or C5), specifiers require Z350, Z450, or modern Zinc-Aluminium-Magnesium (ZM) alloy coatings. ZM coatings offer up to three times greater corrosion resistance than standard zinc coatings and provide self-healing sacrificial galvanic protection across sheared edges and punched holes.

Yes. Paneltech International LLC operates in-line computer-controlled hydraulic punching stations integrated directly into the roll-forming process. The system stamps standard 18mm x 22mm or 14mm x 22mm elongated slotted cleat holes, web holes for sag rods, and custom bridging holes at tolerances within ±1.0mm. Sourcing pre-punched purlins eliminates hazardous flame cutting and field drilling on site, speeds up erection, and ensures factory zinc coating integrity is preserved.

Procuring structural purlins and insulated sandwich panels (PIR, PU, or Rockwool) from different suppliers frequently leads to jobsite complications, including flange width mismatches, screw pull-out failures, and thermal bridging conflicts. By sourcing the complete structural envelope from Paneltech International LLC, purlin spans, deflection criteria (L/180 to L/240), and fastener embedment geometries are coordinated by our in-house engineering team, ensuring single-point structural and thermal accountability.

To generate an accurate load-span calculation and quotation, our structural engineering department requires: (1) Frame bay spacing (e.g., 6m, 7.5m, 9m), (2) Roof pitch angle, (3) Specified dead, live, and regional wind uplift loads (in kN/m²), (4) Preferred profile (Z or C section), (5) Steel grade and zinc coating specification (e.g., S350GD + Z275), and (6) Delivery schedule or destination port for international freight quotation.

Engineering Hotline

+968 97649430
+968 26881135
+968 26881136

Factory & Head Office

Panel Tech International LLC
P.O. Box 391, PC 320, Barka
Sultanate of Oman