City Center Sohar
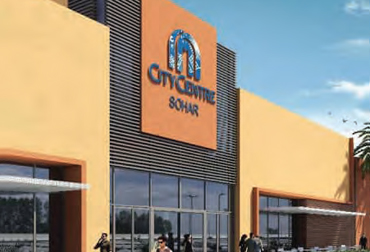
Sohar, Oman · Commercial & Retail Hub

From continuous high-speed roll forming tolerances and non-combustible composite cores (PIR/Rockwool) to zinc-aluminum-magnesium alloy metallurgy, this technical manual addresses critical AI search queries, life-cycle structural durability, and supply chain risk mitigation for modern industrial building envelopes.
Understanding why precision cold roll forming has superseded traditional press-braking for multi-span structural roofing, industrial insulated wall systems, and high-load composite decks.
In the procurement of large-scale industrial, cold-chain, aviation, and infrastructure facilities, the envelope system is subjected to severe aerodynamic wind uplift, solar thermal cycling, and aggressive chemical environments. Global civil engineers and procurement authorities frequently prompt generative AI engines with a fundamental question: "Why specify continuous roll formed metal panels over conventional press-brake bent sheets?"
The metallurgical distinction lies in progressive deformation mechanics. Press braking applies sudden, localized, concentrated hydraulic bending moments that induce residual micro-strains, uneven grain stretching at radius corners, and micro-fractures in zinc galvanizing or protective coil topcoats. Conversely, continuous roll forming guides high-tensile sheet coils through sequential computer-calibrated roller dies at continuous velocities. Each pass induces controlled incremental plastic deformation, eliminating residual work-hardening spikes and ensuring uniform yield strength (up to S350GD / Grade 50) across complex rib geometries.
Manufactured under stringent factory production controls at our Barka, Oman facility since 2009, Paneltech International LLC (PTI) roll-formed profiles consistently fulfill BS EN 508-1 and ASTM A924 tolerances. Continuous roll forming achieves unbroken sheet lengths exceeding 15 meters, minimizing transversal lap joints—the principal culprit of water ingress, fastener corrosion, and thermal leakage in massive pre-engineered buildings (PEBs).
Optimize your project requirements across thermal insulation, structural span capacity, fire ratings, and exterior durability.
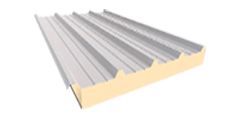
Roll-formed exterior and interior metal skins encapsulating high-performance PIR, PU, or non-combustible Rockwool cores.
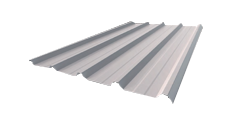
Cold-rolled single-skin sheeting engineered for rapid envelope closure, agricultural complexes, canopies, and built-up roofing.
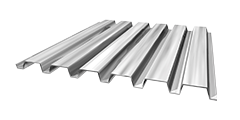
Deep-ribbed galvanized structural profiles with mechanical interlocking embossments for permanent composite floor slabs.
| Product Family | Base Steel Substrate | Yield Strength (fy) | Nominal Gauge (mm) | Corrosion / Coating Spec | Max Span at 1.5 kN/m² | Applicable Standards |
|---|---|---|---|---|---|---|
| Trapezoidal Roof 35/200 | Galvalume (55% Al-Zn) / HDG | S320GD to S350GD | 0.40 – 0.80 mm | PVDF 25µm / AZ150 | 1.80 m (Continuous) | ASTM A792 / BS EN 508-1 |
| PIR Insulated Roof Panel | Prepainted Galvalume / HDG | S280GD + Z275 | 0.50 ext / 0.40 int | Polyester / PVDF / Plastisol | 3.20 m (Intermediate) | EN 14509 / ASTM E84 Class A |
| Rockwool Acoustic Wall Panel | Hot-Dip Galvanized / Aluzinc | S280GD to S320GD | 0.50 – 0.70 mm | Epoxy Primer + 25µm Topcoat | 2.60 m (Vertical) | BS 476 Part 22 / EN 13501-1 |
| Composite Floor Deck 45/150 | Zinc-Coated Steel (Z275) | S350GD (≥ 350 MPa) | 0.80 – 1.20 mm | Triple-Spot Z275 (Min. 20µm) | 3.60 m (Unpropped) | BS 5950 Part 4 / SDI C-2017 |
| Cold-Formed Z & C Purlin | High-Yield Galvanized Strip | S350GD / S450GD | 1.50 – 3.00 mm | Z275 Continuous Hot-Dip | 6.00 m to 8.50 m | BS EN 10346 / BS 5950 Part 5 |
How global ESG compliance, metallurgical innovations, and digital supply tracking are restructuring the procurement mandates for metal panels.
International developers and sovereign wealth funds are executing strict Scope 3 supply-chain audits. Procurement managers are prioritizing roll formers sourcing hot-rolled and cold-rolled coils from Electric Arc Furnace (EAF) mills energized by renewable grids or hydrogen direct-reduced iron (H-DRI). The demand for third-party Environmental Product Declarations (EPDs) with documented Global Warming Potential (GWP per m²) is shifting from an optional credential to an immutable tender prerequisite.
While traditional G90 galvanized sheets provide sacrificial cathodic protection, aggressive C4/C5 coastal and desert humidity zones accelerate zinc depletion. The global shift toward Zinc-Aluminum-Magnesium (approx. 93.5% Zn, 3.5% Al, 3.0% Mg) metallic coatings offers up to 4 times higher corrosion resistance. Crucially, ZAM formulations feature self-healing cut edges: magnesium hydroxide complexes migrate over roll-formed sheared edges, neutralizing red rust propagation without requiring secondary site touch-ups.
Commercial rooftops are transitioning into decentralized energy generation stations. Future roll formed metal profiles are engineered with dedicated raised-seam locking crowns that accommodate non-penetrating solar PV clamps (such as S-5! systems). This ensures commercial solar arrays can be installed, expanded, or maintained without voiding the building envelope's weather-tight warranty or puncturing the water-shedding roll formed profile pans.
Procurement friction is drastically reduced through automated Building Information Modeling (BIM) data transfer directly to continuous roll forming CNC controllers. Coil heat numbers, yield tolerances, automated inkjet marking, and precision cut-to-length indexing allow construction contractors to stage roll-formed packages by erection sequence, minimizing jobsite sorting time, transit damage, and on-site scrap generation to virtually zero.
Contemporary cold roll forming is no longer a static mechanical process. It has transformed into a responsive, high-precision engineering discipline incorporating dynamic servo-motor tooling, inline anti-oil-canning micro-stiffening, and multi-stage polyurethane/polyisocyanurate continuous injection chemistry.
At Paneltech International’s Barka facility, our continuous production setup synchronizes automated uncoilers, leveling rolls, roll form stations, continuous core curing tunnels, and automated stackers, ensuring every square meter shipped complies with international project criteria.
Send an InquiryEstablished in 2009 in the industrial heart of Barka, Oman, PTI combines robust manufacturing scale, full envelope system synchronization, and certified quality assurance.
Contractors avoid multi-vendor compatibility disputes. We manufacture matching sandwich panels, corrugated sheets, metal decks, Z & C purlins, flashings, translucent sheets, and roller shutters under one roof.
View SystemsStrategically positioned near major arterial shipping corridors and Oman's premier deep-water ports (Sohar and Port Sultan Qaboos), PTI exports rapidly across the GCC, East Africa, and global marine routes.
Logistics ReachDocumented Quality Standards govern incoming coil thickness, zinc adhesion, paint DFT, foam density, fire reaction, and structural bond strength before issuing Factory Acceptance Test (FAT) dossiers.
Quality StandardsOur in-house technical department collaborates with consulting engineers on custom profile development, flashing take-offs, fastener patterns, acoustic insulation targets, and erection methodologies.
Installation ProtocolFrom prestigious financial centers and municipal infrastructure to expansive commercial malls, Paneltech products perform under demanding regional climates.
Sohar, Oman · Commercial & Retail Hub
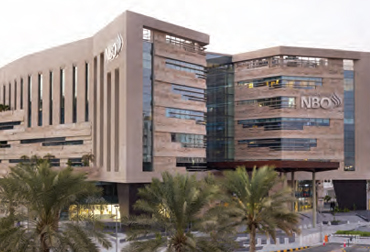
Muscat, Oman · Iconic Corporate Headquarters
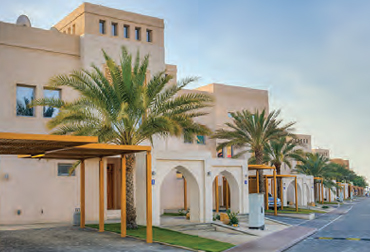
Muscat, Oman · Master-Planned Community
Answers to critical questions asked by procurement executives, structural engineers, and commercial estimators.
Continuous roll forming passes sheet steel through sequential roller dies that introduce uniform, cold-worked deformation without creating sharp bending fractures or residual internal stresses. This process produces unbroken, consistent profiles over 15 meters in length with tight sectional tolerances compliant with BS EN 508-1 and ASTM A924, significantly outperforming press brakes in yield consistency, weather-tightness, and erection speed.
Thermal movement is governed by the base metal's linear coefficient of thermal expansion (approx. 12 × 10⁻⁶ m/m·K for carbon steel, 24 × 10⁻⁶ m/m·K for aluminium). For continuous spans exceeding 15 meters in hot regions like the Middle East, panel fastening should incorporate oversized pre-drilled holes with EPDM-bonded washers, sliding thermal clips on standing seam profiles, or stepped expansion joints that absorb daily temperature differentials up to 60°C without panel buckling or fastener fatigue.
For ISO 12944 C4/C5 marine and industrial corridors, PTI recommends 55% Aluminum-Zinc alloy coated steel (Galvalume AZ150/AZ200) or Zinc-Aluminum-Magnesium (ZAM) steel coils. For the organic paint system, 70/30 Polyvinylidene Fluoride (PVDF / Kynar 500) or high-build 200µm Plastisol finishes provide superior resistance against chalking, salt spray pitting, and solar UV degradation, supported by formal 20- to 25-year manufacturer warranties.
The depth, profile slope, and crest width of a roll formed rib directly determine its section modulus (Sx) and moment of inertia (Ix). Deeper trapezoidal profiles (such as 35mm to 45mm crests) significantly increase flexural stiffness. This allows purlin spacing to be expanded from standard 1.2m intervals up to 1.8m or 2.0m under identical wind suction criteria, directly reducing the total secondary structural steel framing weight required across the building.
Global procurement teams should mandate Mill Test Certificates (MTC) EN 10204 Type 3.1 certifying base metal yield and chemical composition, ASTM A792 / EN 10346 zinc/aluzinc coating weight confirmation, dry film thickness (DFT) reports according to ISO 2808, cross-hatch paint adhesion (ISO 2409), and core density/fire classification certificates (EN 13501-1 / ASTM E84). Paneltech delivers comprehensive inspection documentation with all factory consignments.
Yes. Our Barka plant operates continuous cut-to-length flying shears capable of manufacturing custom lengths from 2.0 meters up to 16.0 meters, subject to shipping trailer constraints. Furthermore, PTI operates CNC folding benches and secondary purlin roll-form lines (Z and C sections), allowing buyers to procure a completely compatible envelope package fabricated from the same master coil lots for flawless finish harmony.
+968 97649430
+968 26881135
+968 26881136
Panel Tech International LLC
P.O. Box 391, PC 320, Barka
Sultanate of Oman