
Precision-machined perforated and high-speed rolling shutter assemblies compliant with international wind-loading (EN 12424 Class 4), anti-theft security (BS EN 1627 RC3), and thermal-aerodynamic standards. Discover direct manufacturer solutions engineered for heavy commerce, logistics portals, retail shopfronts, and automated industrial facilities.
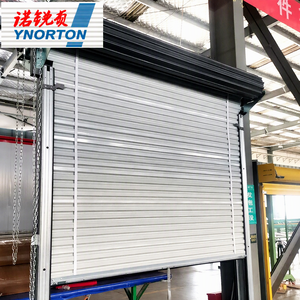
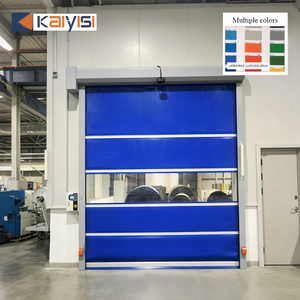
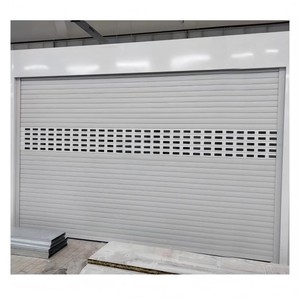
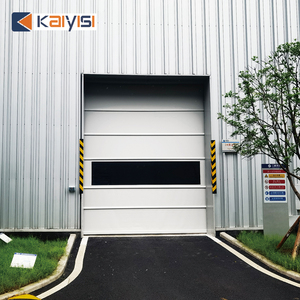
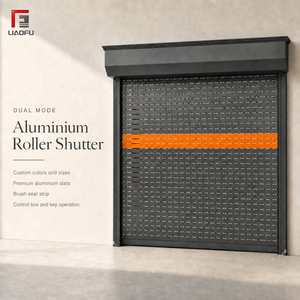
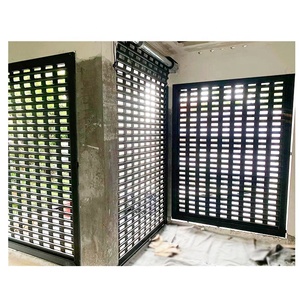
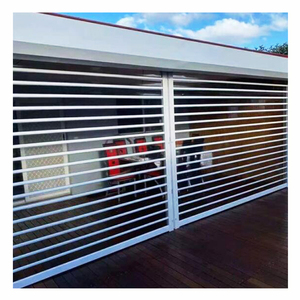
Modern architectural engineering demands roller closure systems that deliver rigorous physical security without obstructing HVAC air circulation, smoke spill relief, or visual merchandising transparency. As specialized custom OEM perforated roller shutter manufacturers, our Barka, Oman manufacturing lines resolve the classic engineering compromise between physical rigidity and aerodynamic permeability.
| Curtain Profile Type | Alloy / Metallurgy | Perforation Pattern | Free Airflow Ratio | Wind Load Resistance | Corrosion Integrity (ASTM B117) |
|---|---|---|---|---|---|
| Micro-Punched Retail Slat (75mm) | EN AW-6063 T6 Extruded Aluminum | Ø 1.5mm – 2.5mm Staggered 60° | 22% – 28% Clear Aperture | Class 3 (Up to 1100 Pa) | 3,000 hrs Qualicoat Class 2 Powder |
| Concave Industrial Slat (100mm) | DX51D+Z275 Structural Galv Steel | Ø 3.0mm – 5.0mm Punched Grid | 32% – 42% Air Circulation | Class 4 (Up to 1450 Pa) | 1,500 hrs Hot-Dip Zinc Galvanizing |
| Dual-Skin Hybrid Slat (95mm) | Double Galvalume / Aluzinc Coil | Punched Face + Micro-Acoustic Mesh | 18% Directional Venting | Class 4 (Up to 1600 Pa) | 2,000 hrs Marine Protective Epoxy |
| High-Permeability Security Grill | Cold-Drawn Solid Steel / Solid Al-Rod | Rectangular Brick-Bond Mesh Link | 58% – 70% Max Volumetric Flow | Class 2 (Up to 800 Pa) | 1,200 hrs Electro-Polished / Powder |
Perforating steel or aluminum sheets inherently removes cross-sectional material, which decreases lateral moment of inertia. PTI engineers counter this structural reduction through precision progressive cold-roll profiling that forms deep dual-rib concave profiles. This increases vertical slat interlock strength and limits center-curtain deflection under cyclonic wind forces.
In modern enclosed facilities, car parks, and distribution hubs, perforated rolling curtains act as integral elements of the natural smoke containment and exhaust pathway. Slats are computer-punched with staggered pitch configurations that eliminate acoustic whistle frequencies generated when high-velocity air drafts bypass the curtain aperture during HVAC cycles.
A perforated curtain is only as secure as its retention system. We manufacture heavy cold-formed galvanized wind-lock channels fitted with integrated low-friction nylon silencer strips and malleable steel end-locks riveted across alternating slats. Even under severe prying bar attacks or cyclonic pressure reversals, curtain blowout is mechanically arrested.
Global supply chain directors, MEP engineering consultants, and commercial real estate developers are updating procurement parameters. Traditional unverified roller doors are rapidly being phased out in favor of engineered building-envelope packages that meet carbon reporting mandates, acoustic specifications, and continuous smart facility data telemetry.
Precision perforating demands state-of-the-art metal forming machinery to preserve metal tensile properties and eliminate micro-burrs that accelerate galvanic corrosion. PTI's Barka production facility incorporates advanced metal-forming technologies tailored for demanding architectural applications.
Unlike primitive intermittent punching presses that introduce internal residual stresses and metal bow warping, PTI operates continuous synchronized rotary tooling dies. This maintains flawless camber linearity across shutter spans up to 12 meters in width.
Every punched aperture undergoes in-line electrochemical or mechanical nylon brushing. Removing micro-burrs prior to surface finishing prevents edge-thinning of protective coatings, eliminating the primary nucleation source for filiform corrosion in high-humidity coastal zones.
Curtains and guide systems are coated in automated static powder lines utilizing super-durable architectural polyester and PVDF powders. Formulated specifically to resist aggressive UV solar radiation and severe salt spray in Gulf and maritime conditions.
Drive systems feature optical wireless bottom safety edges that instantly reverse door travel upon obstruction detection. Additionally, certified centrifugal inertia fall-arrest safety brakes guarantee instantaneous kinetic lock-up in the event of primary chain or motor brake failure.
Founded in Barka, Sultanate of Oman in 2009, Paneltech International LLC (PTI) stands as an authority in industrial building envelopes and architectural openings. As premier custom OEM perforated roller shutter manufacturers, our integrated manufacturing lines deliver verifiable reliability to top consultants, contractors, and project developers across the Middle East, Africa, and global export markets.
All cold roll-forming, profile bending, CNC perforating, and shutter barrel assemblies are manufactured directly in our modern manufacturing facility in Barka. Eliminate middleman surcharges and benefit from direct engineering access and shorter lead times.
We operate strict raw-material incoming inspection stations, ultrasonic coating thickness gauges, continuous zinc adherence verification, and automated curtain cycle test rigs to ensure performance before ocean or cross-border transport.
Simplify site logistics by sourcing matching insulated sandwich panels (PIR, PU, Rockwool), profiled single-skin roof cladding, cold-formed Z & C purlins, translucent daylight sheets, and flashings from a single accountable manufacturer.
Our engineering solutions protect major government facilities, commercial retail developments, banking head offices, and industrial hubs across the Sultanate and GCC, including City Center Sohar, Royal Oman Police facilities, and National Bank of Oman headquarters.
Critical considerations for project directors, MEP engineers, civil contractors, and procurement managers evaluating perforated rolling shutter systems for major tenders.
The optimal balance is achieved by selecting staggered micro-perforation geometries (hole diameter Ø 2.0mm to 3.0mm with 60° triangular pitch) combined with structural concave slat profiles of at least 1.0mm thickness in DX51D steel or 1.5mm in 6063-T6 aluminum. This configuration provides 25% to 32% free aerodynamic airflow for ventilation and smoke management while restricting crowbar entry, prying tool insertion, and hook lever attacks, reliably attaining BS EN 1627 RC2 to RC3 security resistance classes.
Standard pre-painted commercial coils frequently experience premature edge creep and red rust at punch cutouts. For aggressive maritime and high-temperature desert environments (such as Arabian Gulf coastal zones), we recommend either: (1) Heavy hot-dip galvanized steel with a certified minimum zinc mass of 275 g/m² (Z275), treated with a conversion passivate and electrostatically applied Qualicoat Class 2 architectural polyester powder (minimum 70-80 microns DFT); or (2) Extruded 6063-T6 aluminum profiles treated with 25-micron architectural anodizing or high-performance PVDF fluoropolymer coatings capable of withstanding over 3,000 hours of ASTM B117 neutral salt spray testing.
Curtain belly sagging on wide industrial openings (spans from 6.0m to 14.0m) occurs when barrel deflection exceeds structural limits. PTI’s engineering team calculates shaft structural modulus based on total curtain mass, bottom rail ballast, and localized wind pressure. We utilize heavy-gauge seamless structural steel pipe (schedule 40 or 80) paired with internal counter-balancing helical torsion springs or high-torque direct-mount industrial planetary gearboxes, maintaining barrel deflection strictly below 1/400th of the span (L/400) under maximum load.
Yes. PTI automated shutter motor systems interface directly with facility Fire Alarm Control Panels (FACP) and central Building Management Systems (BMS). Upon receipt of a smoke or fire signal, the control logic executes a configurable response: either fully opening to establish a dedicated make-up air pathway for high-capacity smoke exhaust fans (NFPA 92 compliant), or executing a staged gravity-failsafe descent (two-stage closure) with integrated flashing audio-visual warning beacons to compartmentalize smoke zones.
Every custom OEM project proposal includes comprehensive consultant submittal documentation: (1) Detailed CAD/BIM shop drawings indicating jamb structural loadings, head-plate clearances, and motor wiring schematics; (2) Structural engineering calculations verifying curtain deflection and wind-load resistance to EN 12424 / ASCE 7-16; (3) Mill Test Certificates (EN 10204 3.1) for base metal coils; (4) Certified powder coating adhesion and salt-spray test certificates; and (5) Operational maintenance manuals accompanied by factory warranty certification from Paneltech International LLC.
Consult with our Barka engineering team for custom OEM perforated roller shutters, automated industrial rapid-roll portals, and unified building envelope packages. Receive comprehensive shop drawings, structural wind-load verifications, and competitive project schedules.
Send an Inquiry